How to Choose a CNC Laser Cutting Machine in 2026?

Choosing a Cnc Laser Cutting Machine in 2026 means matching cutting performance to real production needs. A machine that looks impressive in a showroom may struggle with your material mix, shift pattern, or floor space. Start with the parts you actually make: their metals, thicknesses, tolerances, and monthly volumes. Small details matter. A 6 mm stainless-steel part and a thin aluminum panel place different demands on the laser source, motion system, and extraction setup.

Market data offers useful context, but it cannot select a machine for your shop. Grand View Research estimated the global laser cutting machine market at about USD 5.2 billion in 2023, with growth projected through 2030. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023. That broader automation trend matters because cutting equipment increasingly needs to work smoothly with loading, handling, and production software. Still, forecasts are not purchase advice. Check the assumptions behind them.

This guide examines the factors buyers should test before requesting a quote: laser power, source type, bed size, cutting accuracy, software, service access, and total operating cost. Ask suppliers to run your own sample material, not just a polished demonstration coupon. Watch the cut edge, inspect dross, and time setup as well as cutting. Then compare warranty terms, consumables, training, and local technician response. A perfect specification sheet can still disappoint. Real output depends on operator skill, maintenance, and process settings, too. The right choice is the machine that reliably fits your parts, people, and production plan—not merely the one with the highest wattage.
How to Choose a CNC Laser Cutting Machine in 2026?

Define Materials, Sheet Thickness, Work Envelope, and Required Throughput

Start with the materials you actually plan to cut, not a machine’s maximum specification. A laser suitable for thin stainless steel may behave differently with reflective metal or coated sheet. That difference matters. List each material, its usual thickness, and the thickest sheet you expect to process regularly. Occasional maximum thickness should not drive every purchase decision.

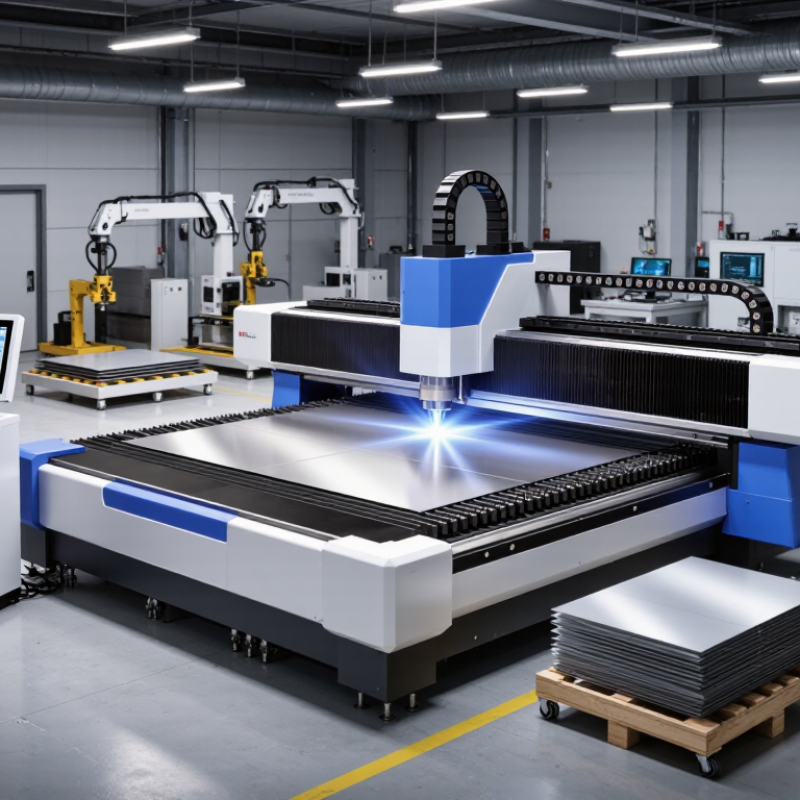
Match the work envelope to real jobs. Measure the largest sheet and parts, including space for loading and removing finished pieces. Allow room for clamps or fixtures if your process uses them. Measure twice. A bed that barely fits a sheet can slow handling and limit nesting options. Also check whether your shop can move and support the machine safely.

Estimate throughput from daily demand, not cutting speed alone. Include setup, material changes, unloading, and routine inspection in your calculations. A shop cutting a few custom panels has different needs from one running repeated batches. If possible, test representative parts at the thicknesses you use most. Record cut quality and cycle time. Initial estimates are often optimistic, so leave some capacity for variation and growth.

Compare Fiber Lasers (~1.07 µm) with CO₂ Lasers (10.6 µm) by Material

Fiber lasers, operating near 1.07 µm, are usually the stronger choice for sheet metal. They cut materials such as mild steel, stainless steel, and aluminum efficiently, often leaving a narrow kerf. Copper and brass can also be cut, but their reflectivity and heat transfer require suitable machine design and settings. That matters.

CO₂ lasers, at 10.6 µm, are often better suited to nonmetals. They can cut acrylic, wood, paper, and many fabrics, producing clean edges when focus and speed are dialed in. Acrylic may show a polished edge; wood can darken or char, especially around tight corners. Material composition varies, so test a small offcut before committing to a full sheet.

The wavelength alone does not determine cut quality. Thickness, assist gas, lens condition, and focus all affect the result. A fiber laser may handle some nonmetals poorly, while a CO₂ laser generally is not the practical option for bare metal cutting. Not always. Coated or composite materials can behave unpredictably, and some release hazardous fumes when processed. Check the material supplier’s safety information and use appropriate extraction. A short test cut can reveal burrs, discoloration, or excess heat before production begins.

Select Laser Power Using Cut Charts for Thickness, Speed, and Assist Gas

A useful laser-power choice starts with the cut chart for your actual material, thickness, and assist gas—not the machine’s maximum rating. Compare the chart’s cutting speed, gas pressure, nozzle size, and focal position for each thickness. For example, a thin mild-steel sheet may run quickly with oxygen, while nitrogen can produce a cleaner edge but requires different pressure and flow. Treat chart values as starting points. Actual results shift with sheet flatness, surface scale, lens condition, and shop air quality.

Ask suppliers for verified chart data across the thicknesses you cut most often, then test coupons at the stated settings. Record speed, kerf, dross, and edge quality. Small details matter. A clean top edge can still hide heavy lower-edge dross. ISO 9013:2017 classifies thermal-cut quality using five tolerance ranges for measures such as perpendicularity and profile height; use those measures to define acceptance, not appearance alone. Avoid selecting power from maximum-thickness claims. More power may improve capacity, but it does not guarantee faster, cleaner production on every gauge. And a chart can be wrong for your shop. Recheck it after changing gas supply, nozzle, or material batch.

Assess Cut Quality Using ISO 9013:2017 Tolerance Classes

When comparing a CNC laser cutting machine, ask for cut samples at the thicknesses and materials you actually use. ISO 9013:2017 classifies thermal-cut quality using measures such as perpendicularity or angularity tolerance, u, and mean profile height, Rz5. Its tolerance ranges depend on material thickness. In general, a lower class number indicates tighter tolerances. Check the standard’s relevant tables rather than treating one class as a universal guarantee.

Inspect a cut edge under consistent lighting, then measure it with suitable inspection tools. Look for taper, roughness, dross, and changes along the cut—not just a clean-looking start. A single coupon can flatter a machine. Ask how the sample was cut, including material, thickness, speed, and assist gas, and request repeat cuts. Small setup changes matter. Compare results with the ISO tolerance range that matches your part requirements, then confirm critical dimensions on your own material. ISO classification helps make comparisons more objective, but it does not replace production trials or prove repeatability across every job. That distinction is easy to miss. A machine may meet a class on one test while your real parts still need adjustment.

How to Choose a CNC Laser Cutting Machine in 2026? — Assess Cut Quality Using ISO 9013:2017 Tolerance Classes

Illustrative comparison of the ISO 9013:2017 perpendicularity or angularity tolerance limit, u, for a 10 mm workpiece. Lower limits indicate tighter geometric tolerance.

Values are calculated from the standard’s thickness-dependent limits at a = 10 mm: Range 1, 0.05 + 0.003a; Range 2, 0.15 + 0.007a; Range 3, 0.4 + 0.01a; Range 4, 0.8 + 0.02a; Range 5, 1.2 + 0.035a. Use the applicable ISO 9013 requirements and measured sample cuts to compare machines; cut quality also depends on material, thickness, process settings, and other specified characteristics.

Verify Laser Safety Against ISO 11553-1:2020 Requirements

When choosing a CNC laser cutting machine in 2026, treat laser safety as a purchase requirement, not an optional extra. Ask the supplier to show how the machine meets the applicable requirements of ISO 11553-1:2020. Confirm the standard’s scope and edition against the machine’s intended use. A certificate or checklist alone is not proof.

Inspect the enclosure and access points during a practical acceptance check. Opening a guarded door should trigger the intended safety response and prevent hazardous laser emission. Check that viewing windows are rated for the laser’s wavelength and power, and that labels, interlocks, and emergency stops are clearly identified. Look for beam paths that could escape during setup or maintenance. Small gaps matter.

Request test records, operating instructions, and a clear explanation of service procedures. Ask who verified the safeguards and whether the verification covers the machine as delivered, including installed options. A tidy enclosure can still conceal weak procedures. That is easy to miss. Confirm how the machine handles faults, bypass attempts, and routine cleaning. Extraction and fire controls also deserve attention, though they do not replace laser-specific safeguards. If a detail is unclear, pause the purchase and seek review from a competent safety professional.

How to Choose a CNC Laser Cutting Machine in 2026? — Verify Laser Safety Against ISO 11553-1:2020 Requirements

Selection Dimension What to Check Evidence to Request or Verify Practical Decision Guidance
Applicable safety standard Confirm that the machine’s laser-processing safety assessment addresses ISO 11553-1:2020, “Safety of machinery — Laser processing machines — Part 1: Laser safety requirements.” Request the safety assessment, applicable standards list, and conformity documentation for the exact machine configuration being purchased. Check the standard’s applicability and edition with the supplier and your local compliance specialist. A standards reference alone is not proof that the machine complies.
Process and material suitability Match the laser type and available power range to the materials, thicknesses, cut quality, and production volume in your actual workload. Request documented cutting tests using representative material grades and thicknesses, including the specified assist gas and process settings. Compare cut quality, cycle time, edge condition, and operating cost using the same test conditions across candidate machines.
Work area and machine configuration Check the usable bed size, axis travel, loading method, enclosure arrangement, and any openings or options that affect safeguarding. Review the layout drawing and safety documentation for the delivered configuration, including optional doors, pass-throughs, and material-handling equipment. Choose a work envelope that accommodates routine jobs without requiring unsafe access or unassessed modifications.
Laser enclosure and access control Verify that the guarding is designed for the machine’s laser radiation and that access points are addressed in the safety design. Request information on enclosure construction, access-door safeguards, and the machine’s laser emission classification under the applicable classification requirements. Do not assume that an enclosure or a “Class 1” description proves suitability by itself. Verify the classification and safeguards for the complete machine as supplied.
Interlocks and safety functions Check how opening an access point affects laser emission and whether the safety functions are designed and validated for the machine’s risks. Request the safety-function description, validation records, and instructions for checking interlocks during commissioning and periodic maintenance. Reject unclear or undocumented bypass arrangements. Any special operating or service mode should have defined safeguards and procedures.
Viewing windows and observation Confirm that any viewing window or viewing panel is suitable for the laser radiation and operating conditions for which it is provided. Request the window’s documented protective specification and installation instructions, including any limits on use or replacement. Do not substitute ordinary glazing or an unverified viewing panel. Confirm that replacement parts preserve the documented protection.
Warning indicators and labels Check that laser emission status is communicated clearly and that required warnings and labels are present and legible. Inspect the machine, operator instructions, and safety documentation for emission indications, warning labels, and relevant laser information. Indicators and labels support safe operation but do not replace enclosure, guarding, interlocks, or operating procedures.
Beam path and reflected radiation Review how the machine contains the beam during normal operation and addresses foreseeable reflections from the workpiece and surrounding surfaces. Ask for the documented risk assessment and information on beam containment, beam stops or terminations, and restrictions on reflective materials. Confirm that the safeguards cover the intended materials and process conditions, not only a standard test material.
Fume extraction and fire risk Assess extraction capacity and filtration needs for the materials being cut, along with safeguards for sparks, hot parts, and fire. Request extraction and filtration specifications, material restrictions, cleaning instructions, and the machine’s fire-risk control measures. Size the extraction system for the actual process and facility. Check local requirements for the handling and disposal of collected dust or residues.
Controls, software, and operating modes Review operator controls, emergency stopping arrangements, access permissions, and the behavior of automatic, setup, and service modes. Request operating instructions that describe modes, safe setup, fault response, emergency procedures, and protection against unauthorized changes where applicable. Include the control system and software options in the safety review; assess the delivered configuration rather than relying on a generic product description.
Maintenance and service access Check how the machine is made safe for cleaning, alignment, fault finding, and component replacement. Review lockout and isolation instructions, service procedures, training requirements, and any conditions under which guards may be opened. Ensure that routine maintenance can be carried out using documented procedures and that service access does not depend on informal interlock bypassing.
Installation and site integration Account for electrical supply, ventilation, cooling, compressed gas, machine layout, access routes, and connection to external automation. Obtain installation requirements and review the safety impact of conveyors, robotic loading, remote controls, or other connected equipment. Have the completed installation and integrated system assessed before production use; site changes can affect the original safety assumptions.
Documentation and commissioning Confirm that operators and maintainers will receive complete, understandable information for the exact machine configuration. Check for operating and maintenance instructions, risk-related information, safety inspection procedures, training materials, and commissioning records. Make acceptance conditional on reviewing the documents and verifying safeguards during commissioning, rather than relying solely on a sales specification.

Procurement note: This table is a screening aid, not a substitute for the full ISO 11553-1:2020 text, a machine-specific risk assessment, or applicable national regulations. Verify the complete machine and its intended use with a qualified safety professional.